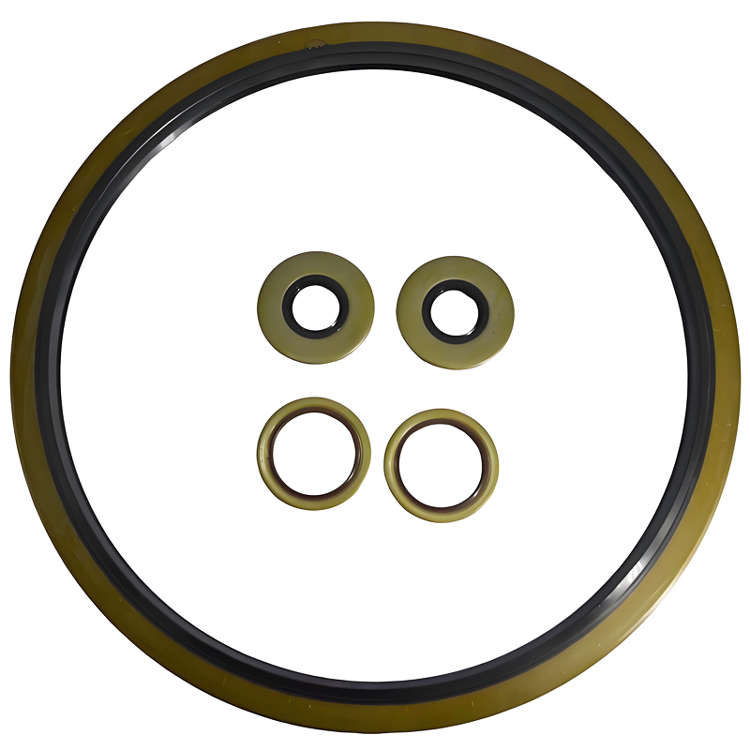
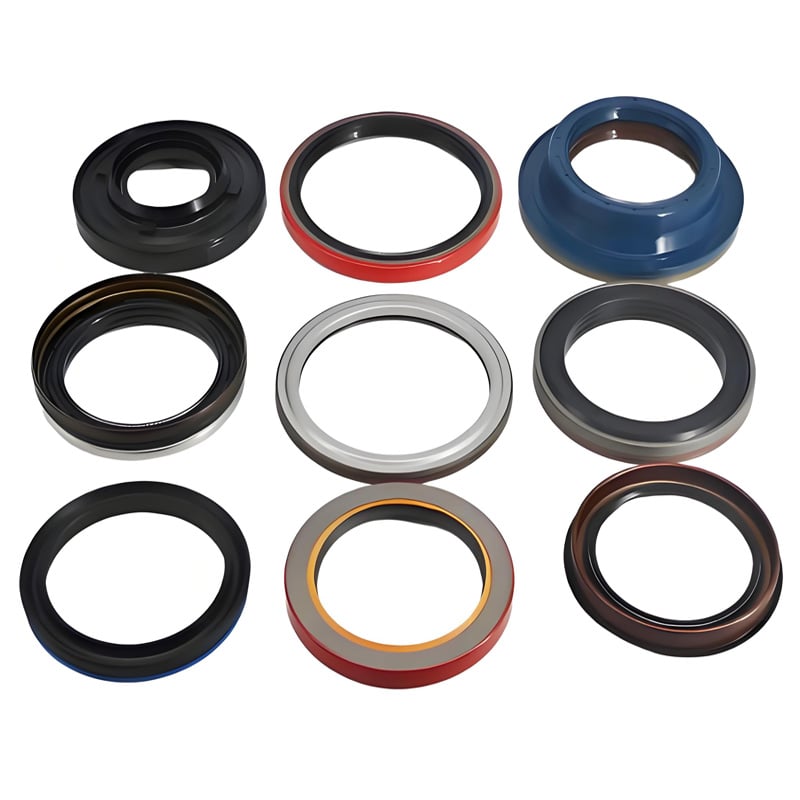
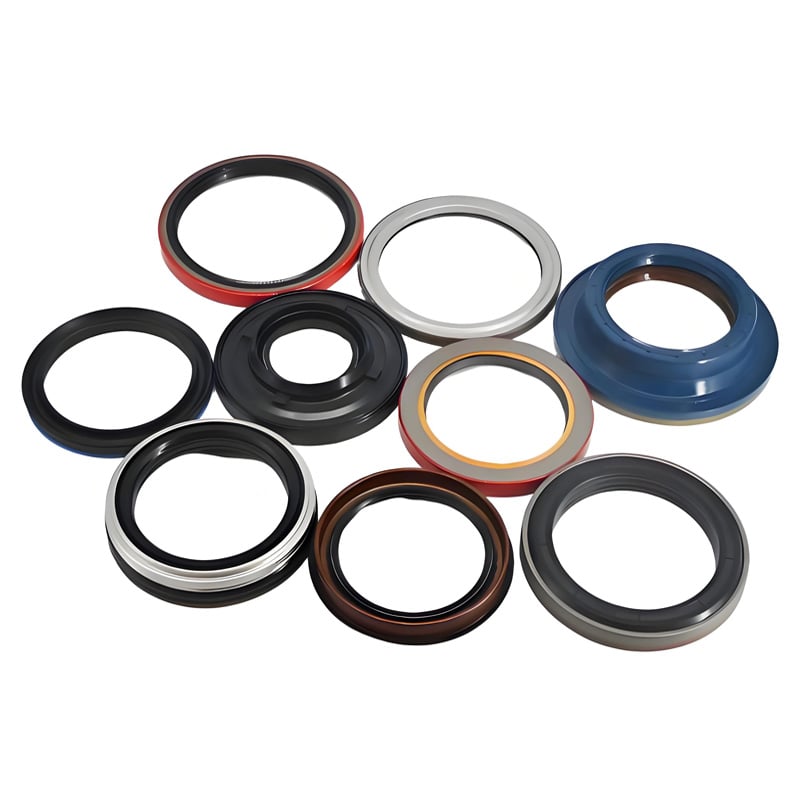
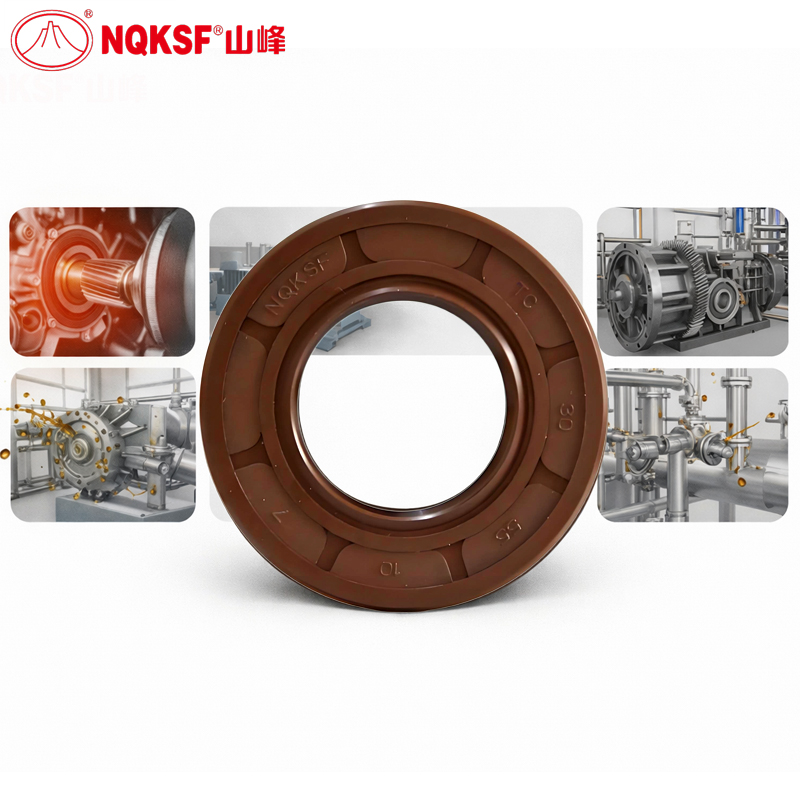
oil seal rubber
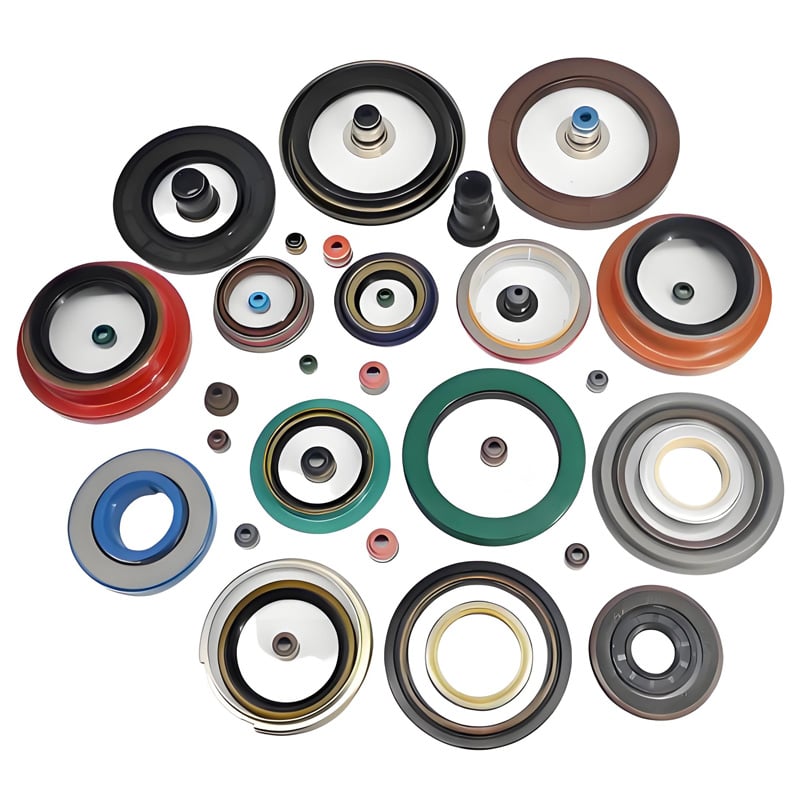
Oil seal rubber is a critical component designed to prevent fluid leakage and contamination in mechanical equipment and machinery. This specialized sealing material serves as a protective barrier between rotating and stationary parts, maintaining system integrity and performance. The primary function of oil seal rubber is to contain lubricating oils, hydraulic fluids, and other essential liquids within designated compartments while preventing external contaminants from entering sensitive areas.
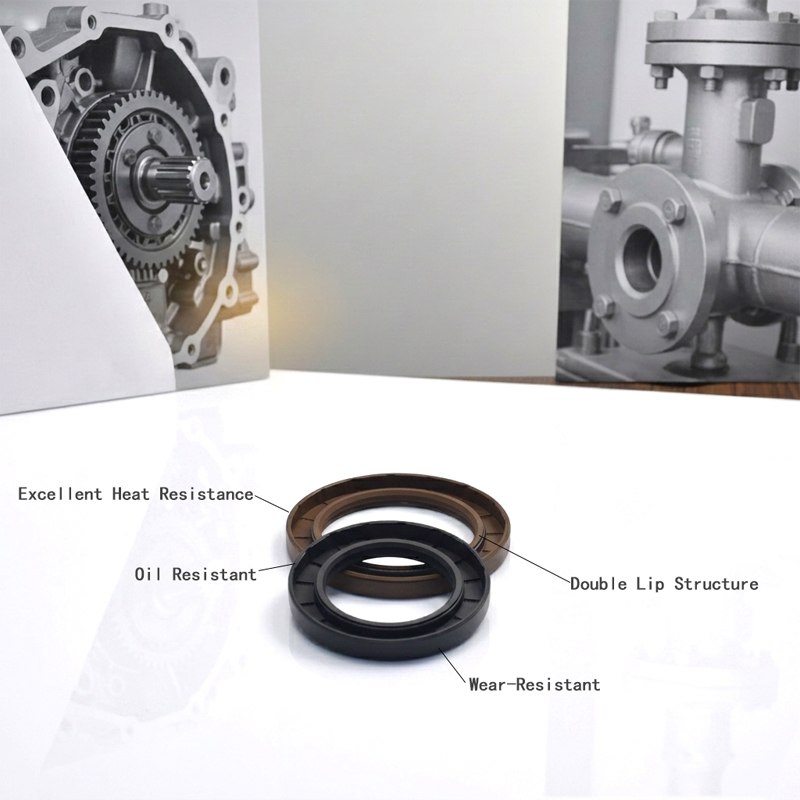
Modern oil seal rubber features advanced technological properties that enhance durability and reliability. The material combines elastomeric compounds with precision engineering to withstand extreme temperatures, pressure variations, and constant mechanical stress. Oil seal rubber components are manufactured using high-grade synthetic and natural rubber materials that provide excellent chemical resistance and flexibility. The sealing surface is engineered with micro-texturing to optimize contact with shaft surfaces, ensuring consistent performance across diverse operating conditions.
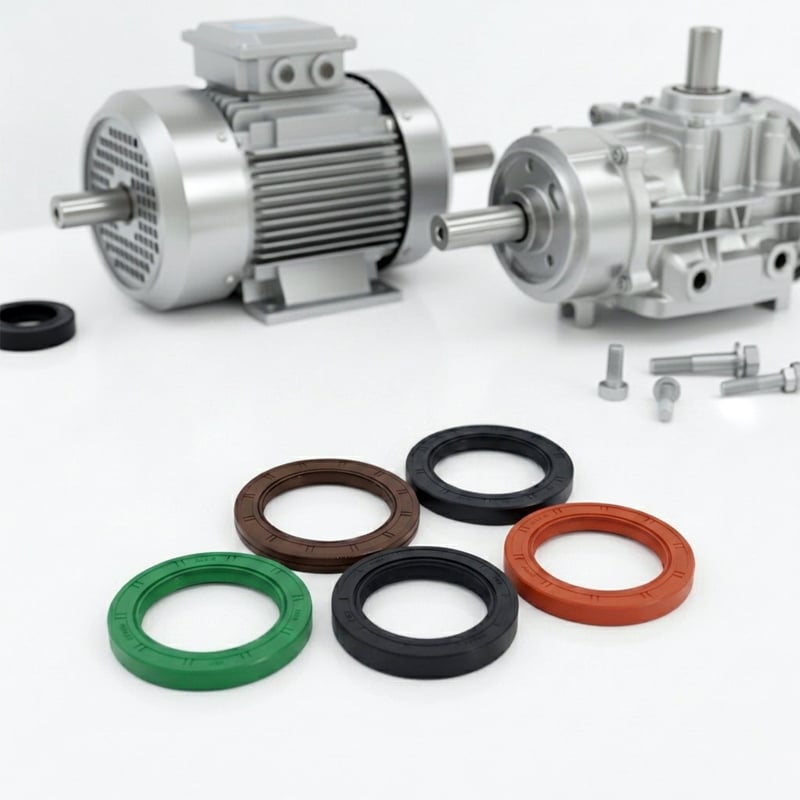
Applications of oil seal rubber span numerous industries including automotive, industrial machinery, hydraulic systems, and rotating equipment. These seals are essential in engines, transmissions, pumps, compressors, and electric motors. Oil seal rubber maintains operational efficiency by reducing friction-related heat generation and preventing costly fluid loss. Industries rely on oil seal rubber to extend equipment lifespan, reduce maintenance frequency, and improve overall system performance. Whether in heavy industrial applications or precision machinery, oil seal rubber delivers dependable sealing solutions that protect investments and ensure continuous operation.
 EN