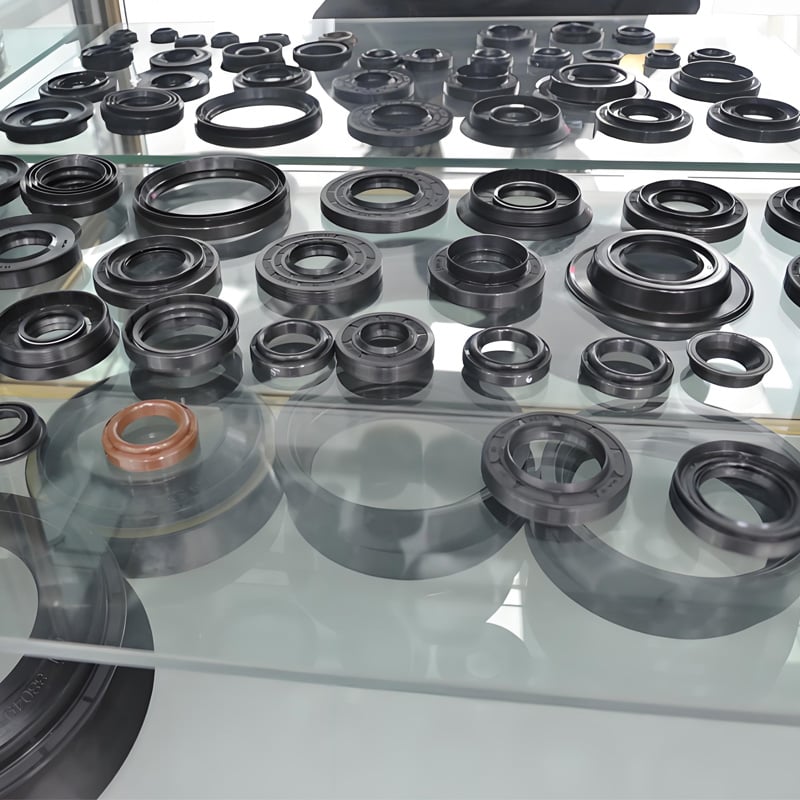
industrial rubber seals
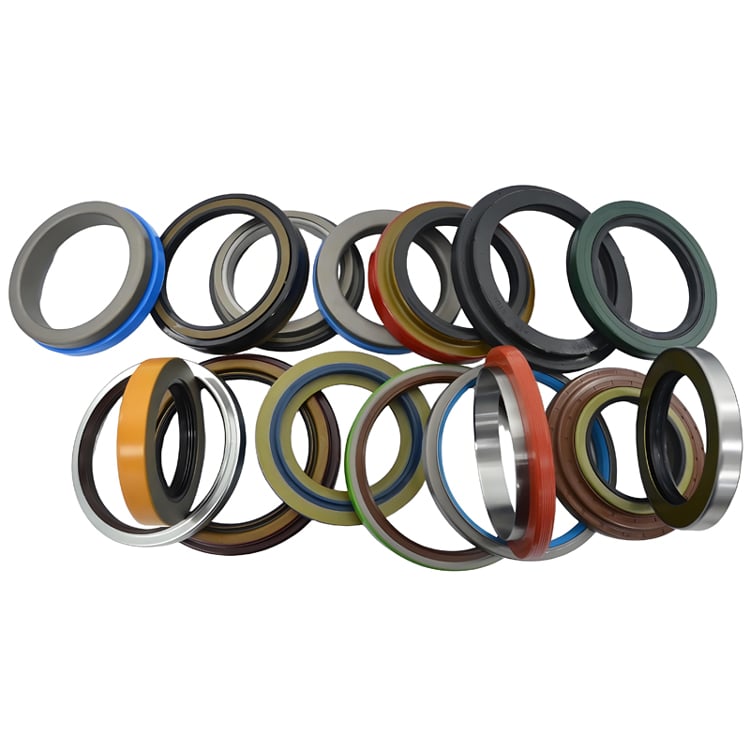
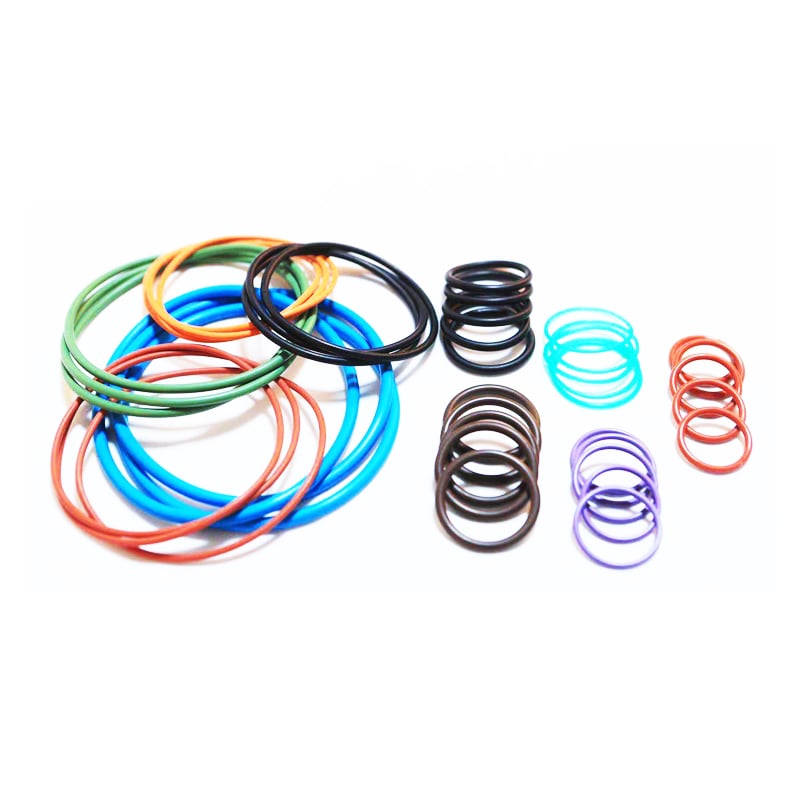
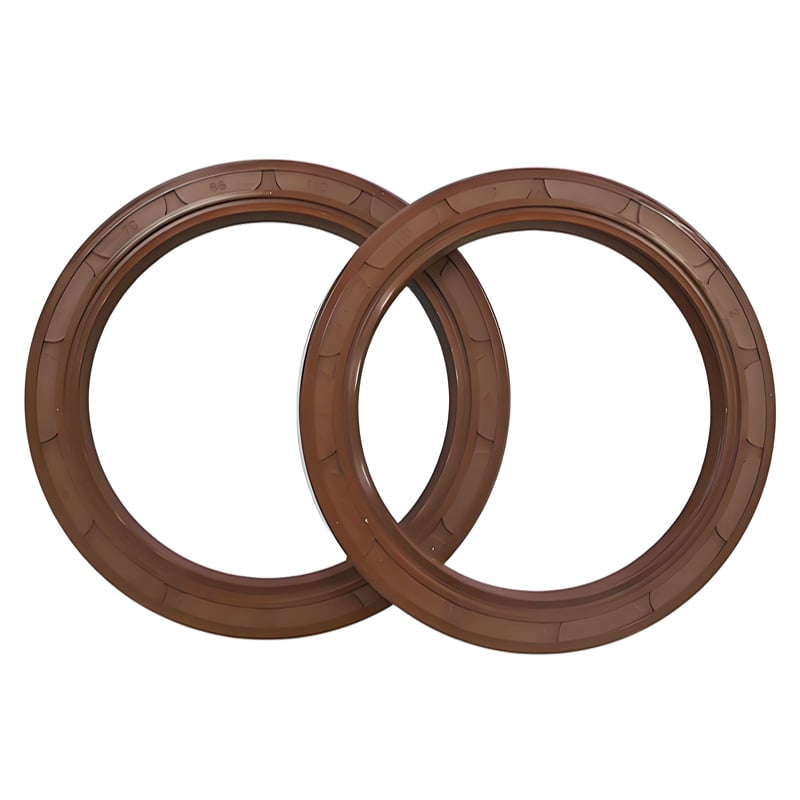
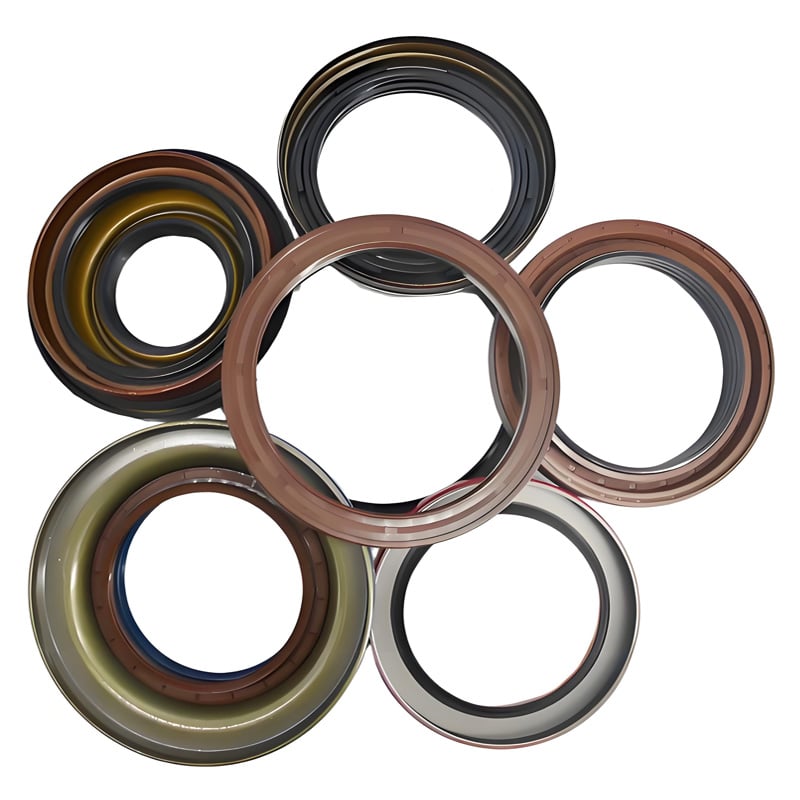
Industrial rubber seals are essential components designed to prevent leakage and contamination in machinery, equipment, and systems across various industries. These precision-engineered seals create reliable barriers that maintain system integrity under demanding operational conditions. Industrial rubber seals function by creating tight barriers between moving or stationary surfaces, effectively blocking fluids, gases, and contaminants from escaping or entering sealed spaces.
The technological features of industrial rubber seals include advanced elastomer formulations, precision manufacturing tolerances, and specialized designs tailored for specific applications. These seals accommodate extreme temperatures, aggressive chemicals, high pressures, and continuous motion without compromising performance. Material selection is critical, with options ranging from natural rubber to synthetic compounds like EPDM, Viton, and nitrile, each offering unique resistance properties.
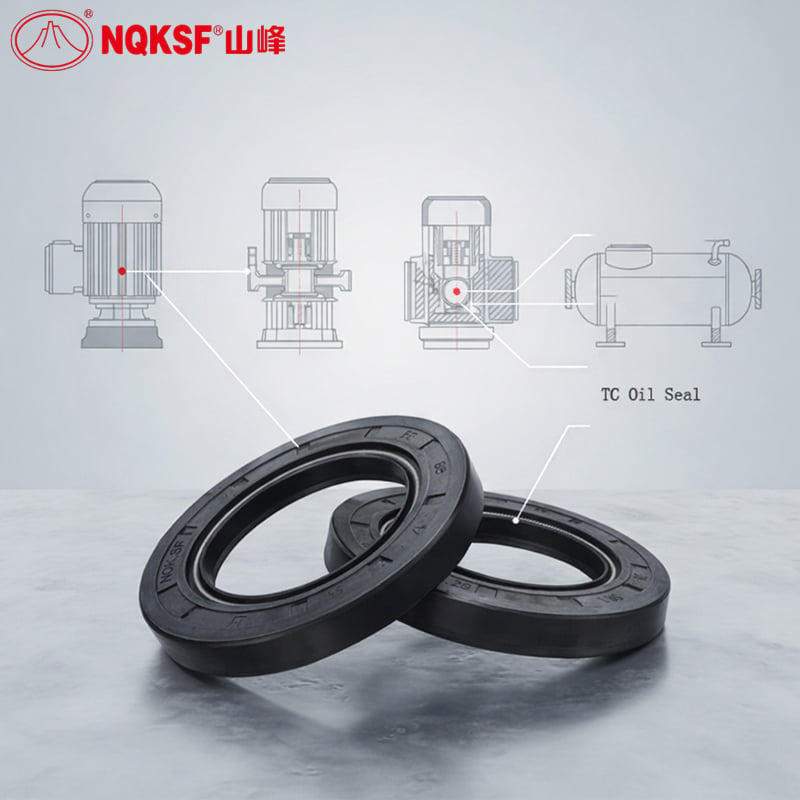
Industrial rubber seals find applications across manufacturing, automotive, hydraulics, pneumatics, food processing, pharmaceutical production, and petrochemical industries. They protect pumps, compressors, cylinders, and rotating equipment from wear and environmental damage. Whether preventing hydraulic fluid leakage in heavy machinery or maintaining sterile conditions in pharmaceutical processing, industrial rubber seals deliver consistent, dependable performance. Modern industrial rubber seals incorporate advanced engineering to meet ISO standards and industry-specific certifications, ensuring compatibility with diverse fluid types and environmental conditions while extending equipment lifespan and reducing maintenance costs significantly.
 EN