Industrial Rubber Seals

All Categories

industrial rubber seals

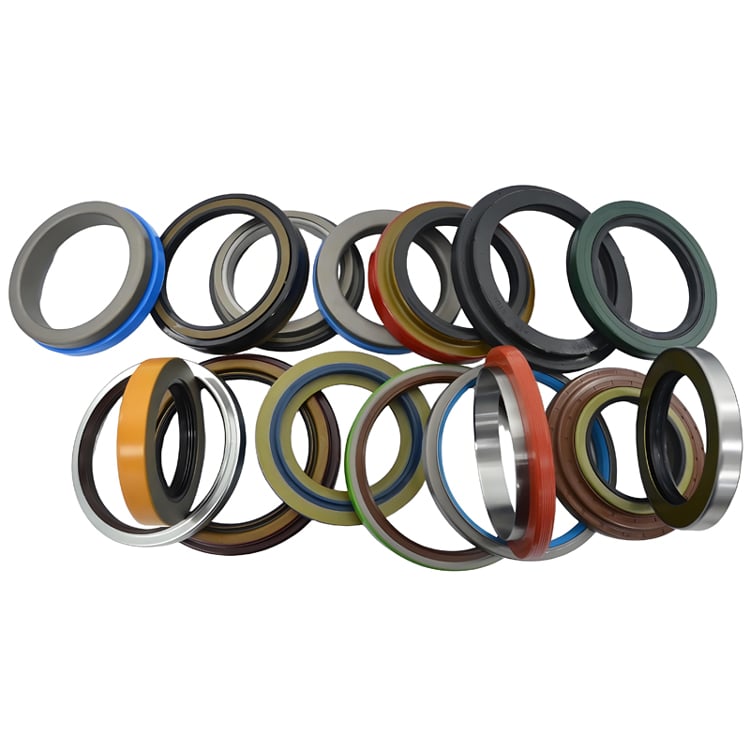
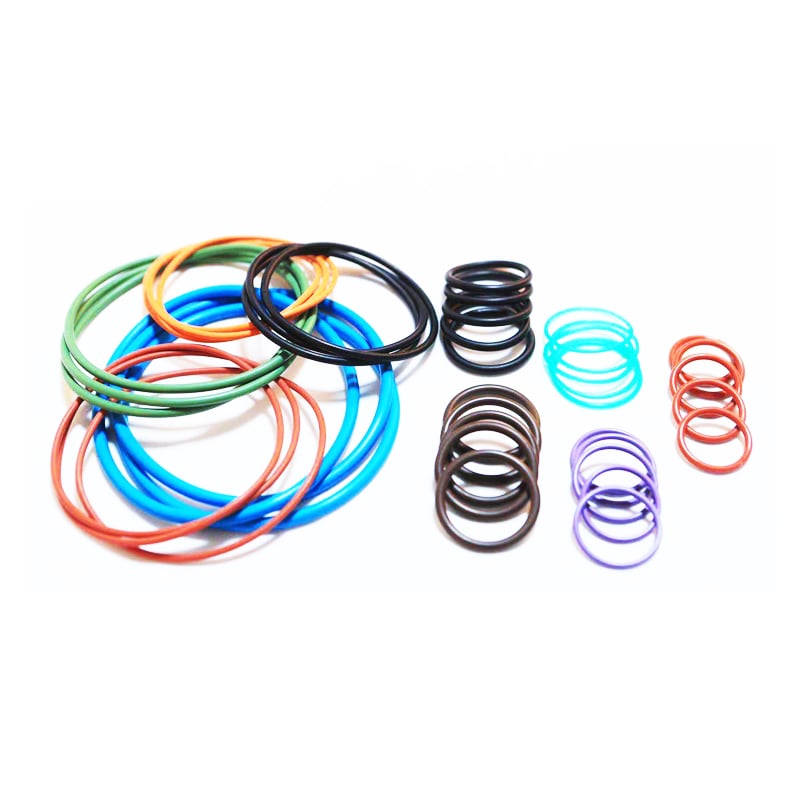
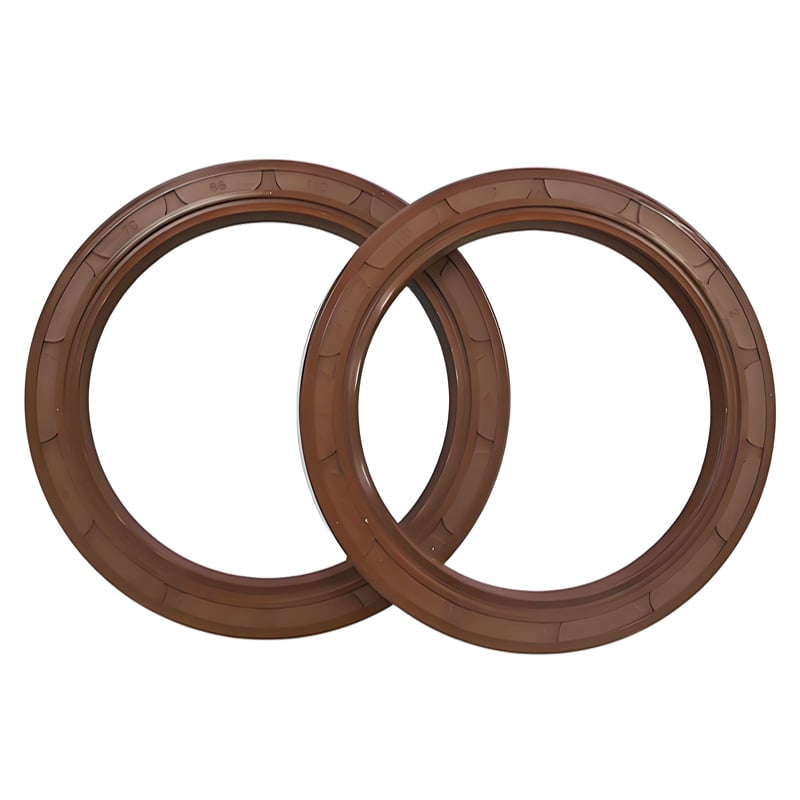
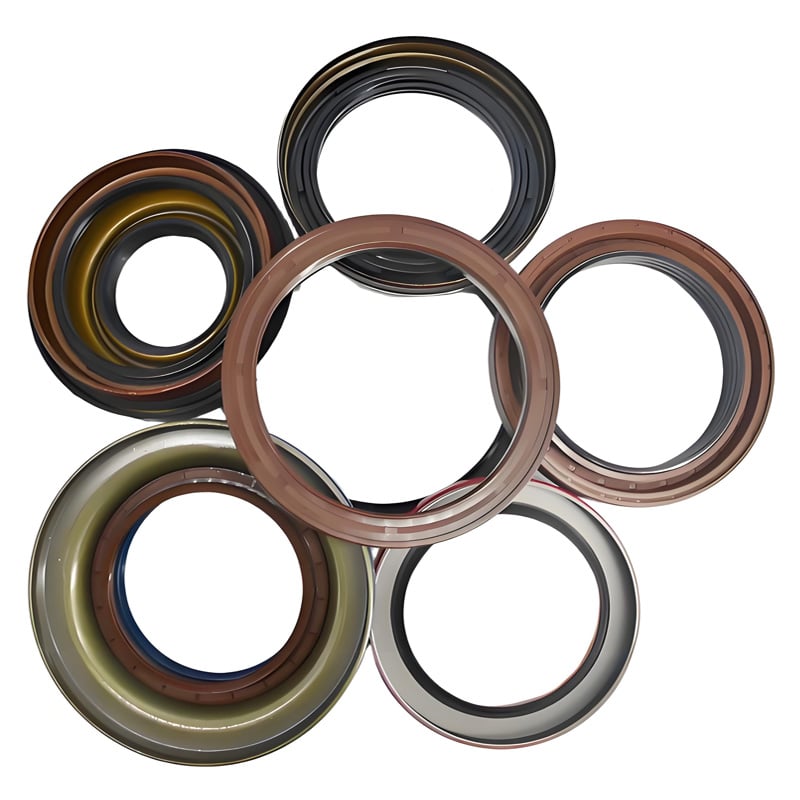
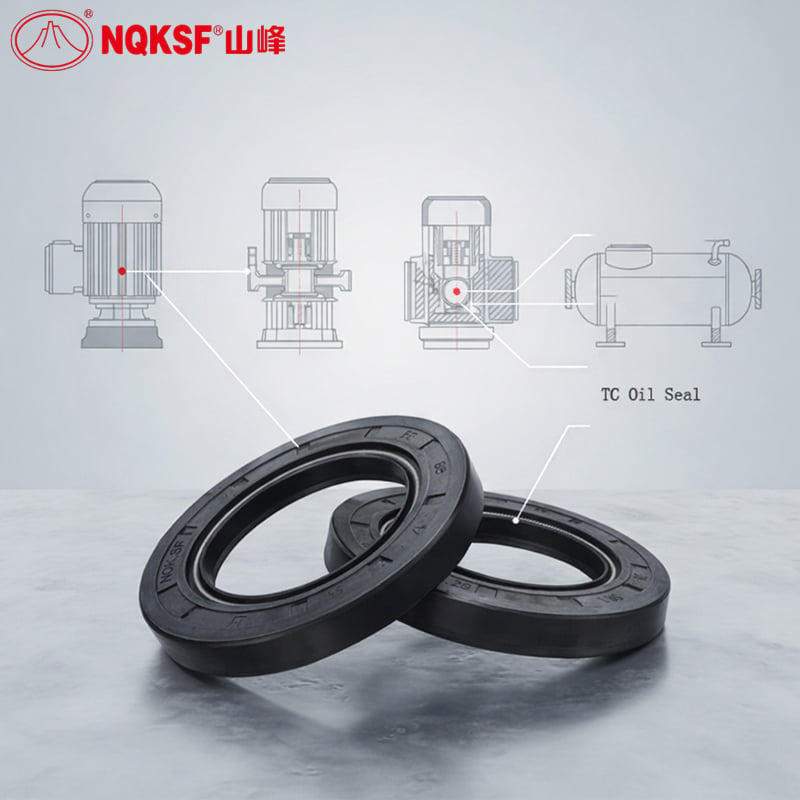
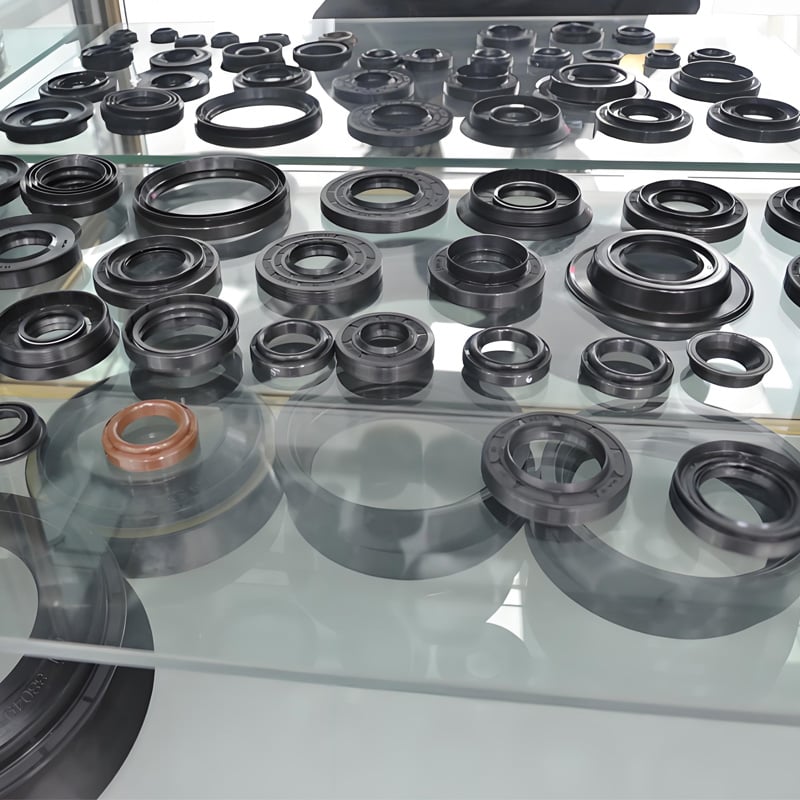
Industrial rubber seals are essential components designed to prevent leakage and contamination in machinery, equipment, and systems across various industries. These precision-engineered seals create reliable barriers that maintain system integrity under demanding operational conditions. Industrial rubber seals function by creating tight barriers between moving or stationary surfaces, effectively blocking fluids, gases, and contaminants from escaping or entering sealed spaces. The technological features of industrial rubber seals include advanced elastomer formulations, precision manufacturing tolerances, and specialized designs tailored for specific applications. These seals accommodate extreme temperatures, aggressive chemicals, high pressures, and continuous motion without compromising performance. Material selection is critical, with options ranging from natural rubber to synthetic compounds like EPDM, Viton, and nitrile, each offering unique resistance properties. Industrial rubber seals find applications across manufacturing, automotive, hydraulics, pneumatics, food processing, pharmaceutical production, and petrochemical industries. They protect pumps, compressors, cylinders, and rotating equipment from wear and environmental damage. Whether preventing hydraulic fluid leakage in heavy machinery or maintaining sterile conditions in pharmaceutical processing, industrial rubber seals deliver consistent, dependable performance. Modern industrial rubber seals incorporate advanced engineering to meet ISO standards and industry-specific certifications, ensuring compatibility with diverse fluid types and environmental conditions while extending equipment lifespan and reducing maintenance costs significantly.
New Products

Industrial rubber seals offer substantial practical benefits that directly impact operational efficiency and equipment longevity. The primary advantage is cost-effectiveness—these seals prevent expensive fluid leaks and system failures, reducing downtime and emergency repairs that disrupt production schedules. By containing fluids and protecting internal components from external contaminants, industrial rubber seals extend equipment lifespan dramatically, maximizing return on investment. Operational benefits are significant and measurable. Industrial rubber seals maintain consistent system pressure, improve machine efficiency, and reduce energy consumption by preventing leakage losses. Equipment operates smoothly with minimal friction-related wear, translating to lower maintenance frequency and reduced labor costs. This reliability proves invaluable in continuous-operation industries where downtime carries substantial financial penalties. Application suitability makes industrial rubber seals versatile across diverse environments. Whether exposed to extreme heat in automotive engines, caustic chemicals in industrial plants, or sterile conditions in food processing facilities, these seals perform reliably. Their adaptability to different pressure ranges, temperatures, and chemical exposures eliminates the need for multiple specialized sealing solutions. For purchasing decisions, industrial rubber seals represent intelligent investments in equipment protection. They prevent costly environmental contamination, reduce regulatory compliance risks, and eliminate unexpected equipment failures. The variety of material compositions allows precise matching to specific operational requirements. Organizations benefit from reduced inventory complexity by standardizing on quality industrial rubber seals that perform across multiple applications, ultimately improving operational predictability and financial performance while enhancing workplace safety and environmental protection standards.

Practical Tips

Which materials are best for a high temperature oil seal in furnaces?

11

Aug

Which materials are best for a high temperature oil seal in furnaces?

Selecting the right materials for a high temperature oil seal in furnaces is critical to ensuring operational reliability and extending equipment lifespan. Furnace environments expose seals to extreme thermal stress, mechanical pressure, and chemical...
View More
Which rotary shaft seal design is best for heavy-duty construction?

25

Aug

Which rotary shaft seal design is best for heavy-duty construction?

Selecting the right rotary shaft seal for heavy-duty construction environments requires understanding how different designs perform under extreme pressure, temperature fluctuations, and contamination exposure. Heavy-duty equipment operates in conditi...
View More
What Are the Key Applications of Shaft TC Oil Seals?

29

May

What Are the Key Applications of Shaft TC Oil Seals?

Shaft TC oil seals serve as critical sealing components in rotating machinery applications across countless industries, where their primary function involves preventing lubricant leakage while blocking external contaminant ingress. These precision-en...
View More
How Do TC Oil Seals Compare to Other Seal Types?

03

Jun

How Do TC Oil Seals Compare to Other Seal Types?

Understanding the differences between TC oil seals and other seal types is crucial for engineers and maintenance professionals selecting the right sealing solution for their applications. TC oil seals, also known as rotary shaft seals or lip seals, r...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Telephone
Name
Company Name
Message
0/1000

industrial rubber seals

Superior Leak Prevention and System Protection

Superior Leak Prevention and System Protection

Industrial rubber seals excel at preventing leakage, protecting valuable fluids, and maintaining system integrity under challenging conditions. Advanced sealing geometry combined with precision elastomer formulations creates impenetrable barriers that contain pressurized fluids reliably. This leak prevention capability proves essential in hydraulic systems, pneumatic controls, and fluid transfer applications where even minor losses compromise performance or create safety hazards. The protective value extends beyond leak containment. Industrial rubber seals shield internal components from external contamination, moisture, dust, and corrosive substances that accelerate wear and component failure. By maintaining clean operating environments within sealed systems, these seals reduce particle generation, extend fluid service life, and prevent costly internal damage. Industries handling sensitive processes—pharmaceutical manufacturing, food production, and precision machinery—depend on industrial rubber seals to maintain product quality and operational safety. This comprehensive protection translates to fewer emergency repairs, extended equipment intervals, and predictable maintenance schedules that support business continuity.
Exceptional Durability Across Demanding Environments

Exceptional Durability Across Demanding Environments

Industrial rubber seals demonstrate remarkable durability when exposed to extreme temperatures, aggressive chemicals, and high-pressure environments that challenge conventional materials. Premium elastomer formulations like Viton and EPDM resist thermal cycling, ozone exposure, UV degradation, and chemical attack from oils, refrigerants, solvents, and process fluids. This material performance ensures industrial rubber seals maintain consistent sealing properties throughout their operational lifespan, even under severe stress conditions. Durability advantages compound over extended service periods. Equipment operators enjoy extended maintenance intervals, fewer emergency seal replacements, and reduced supply chain disruptions. Industrial rubber seals can function reliably for years without replacement, delivering predictable performance that supports equipment uptime and production continuity. The resistance to environmental degradation proves particularly valuable in outdoor equipment, mobile machinery, and process systems exposed to variable conditions. By selecting industrial rubber seals engineered for specific environmental challenges, organizations minimize unplanned failures and associated production losses while reducing total cost of ownership through extended seal life and optimized maintenance planning.
Versatile Design Solutions for Diverse Applications

Versatile Design Solutions for Diverse Applications

Industrial rubber seals come in numerous configurations—O-rings, gaskets, shaft seals, rod seals, and custom profiles—enabling precise solutions for virtually any sealing challenge. This design versatility allows engineers to specify industrial rubber seals that match exact equipment requirements, pressure ratings, fluid compatibility, and installation constraints. Whether requiring radial seals for rotating shafts, static gaskets for flanged connections, or dynamic seals for reciprocating motion, specialized industrial rubber seals exist for every application. Design flexibility extends to material selection and customization options. Organizations can specify industrial rubber seals formulated for temperature ranges from cryogenic to extreme heat, chemical resistance tailored to specific process fluids, and durability enhanced for high-cycle or continuous-duty applications. Custom dimensions accommodate non-standard equipment or legacy system integration. This adaptability eliminates costly equipment modifications or expensive seal replacement procedures. Engineers simplify procurement by standardizing on quality industrial rubber seals across multiple applications, reducing inventory complexity while ensuring consistent performance and compatibility throughout equipment portfolios.

Get a Free Quote

Our representative will contact you soon.
Email
Telephone
Name
Company Name
Message
0/1000