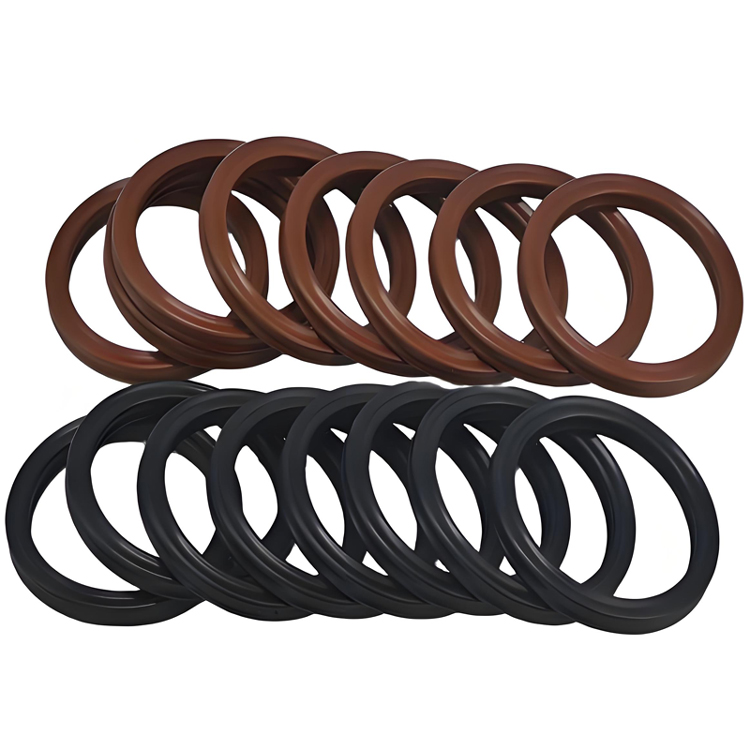
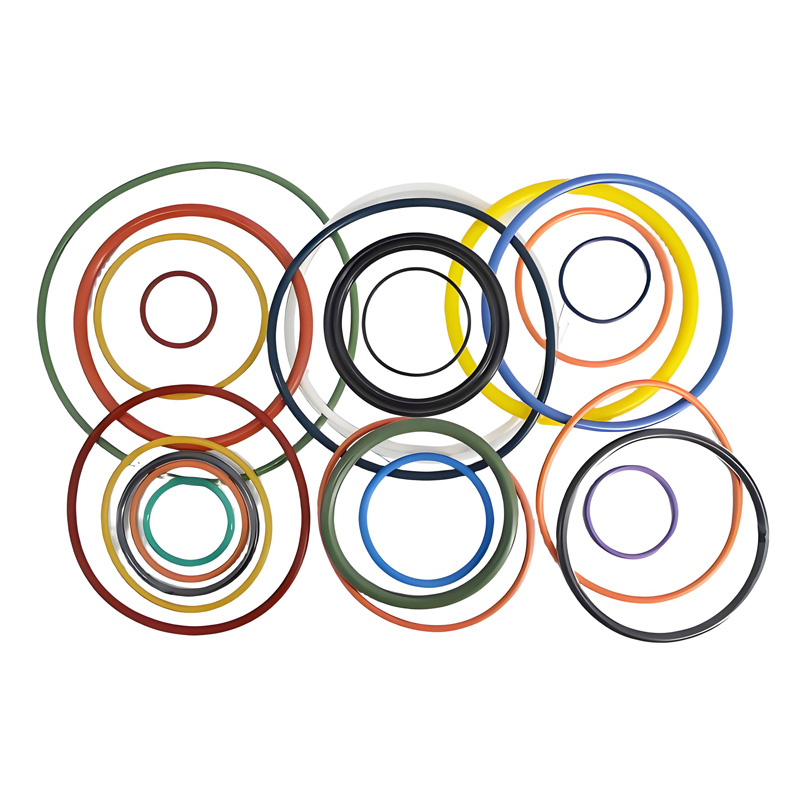
sealing rubber ring
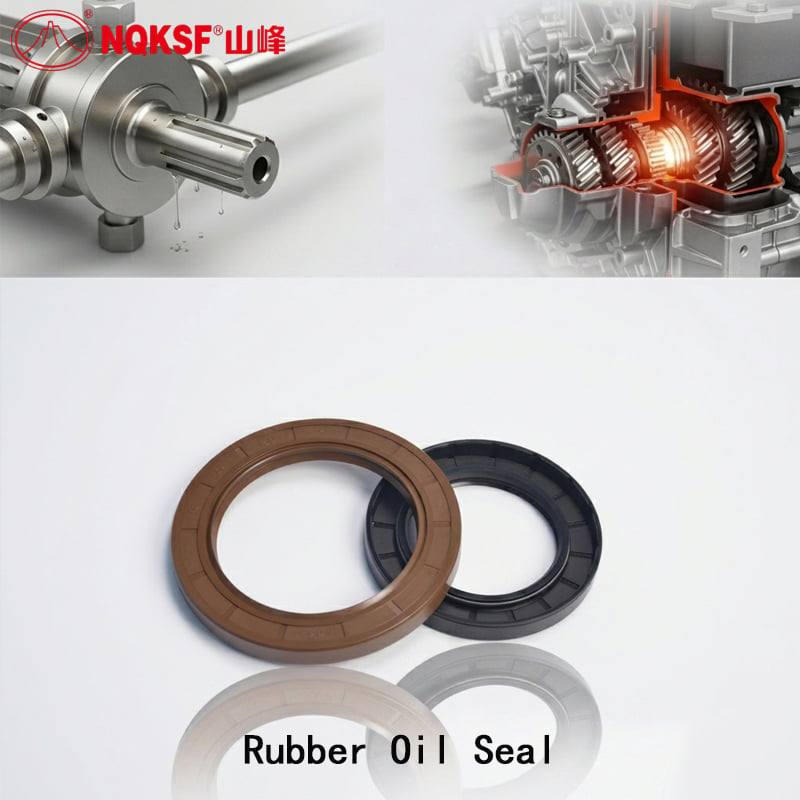
A sealing rubber ring is an essential component designed to create a tight, dependable barrier between two surfaces, preventing liquid or gas leakage in various applications. This sealing rubber ring functions as a critical protective element in mechanical systems, industrial equipment, and domestic appliances. The primary purpose of a sealing rubber ring is to maintain system integrity by blocking unwanted fluid escape or external contamination entry.
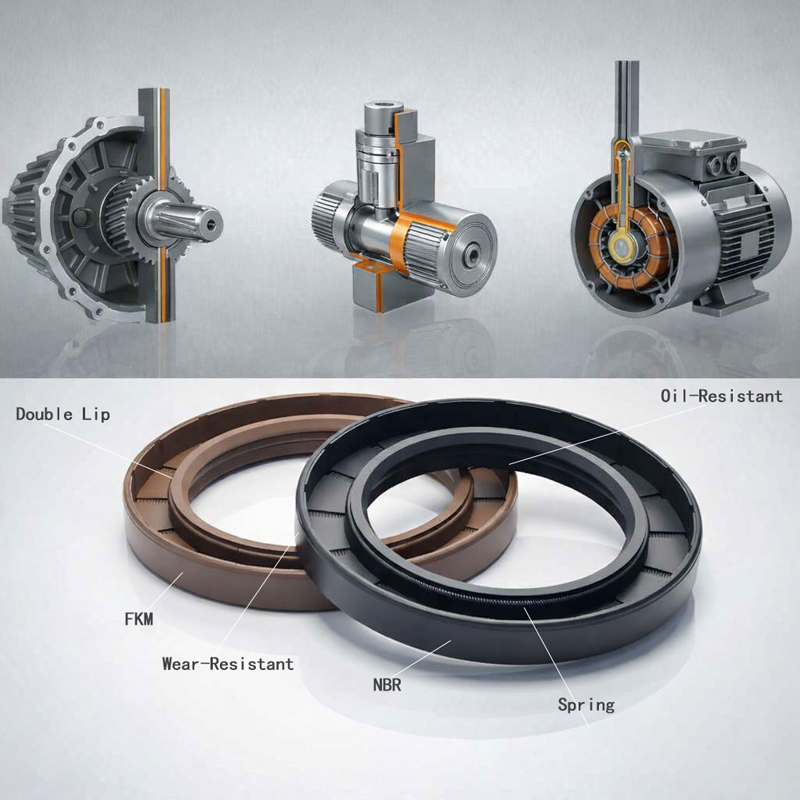
Modern sealing rubber ring technology incorporates advanced elastomer materials that withstand extreme temperatures, pressure variations, and aggressive chemical environments. The technological features of a quality sealing rubber ring include superior elasticity, exceptional durability, and resistance to degradation. Manufacturers engineer each sealing rubber ring with precision dimensions to ensure perfect fit and maximum sealing efficiency across diverse operating conditions.
Applications for a sealing rubber ring span numerous industries. Automotive manufacturers rely on sealing rubber rings in engines, transmissions, and hydraulic systems. Medical device producers use specialized sealing rubber rings to maintain sterility and functionality. Water treatment facilities depend on sealing rubber rings to prevent contamination. Refrigeration units, pumps, compressors, and industrial machinery all require sealing rubber rings for optimal performance. The versatility of sealing rubber rings makes them indispensable in plumbing, HVAC systems, and food processing equipment, where maintaining sealed environments is critical for safety and operational success.
 EN