Sealing Rubber Ring | Professional Leak Prevention

All Categories

sealing rubber ring

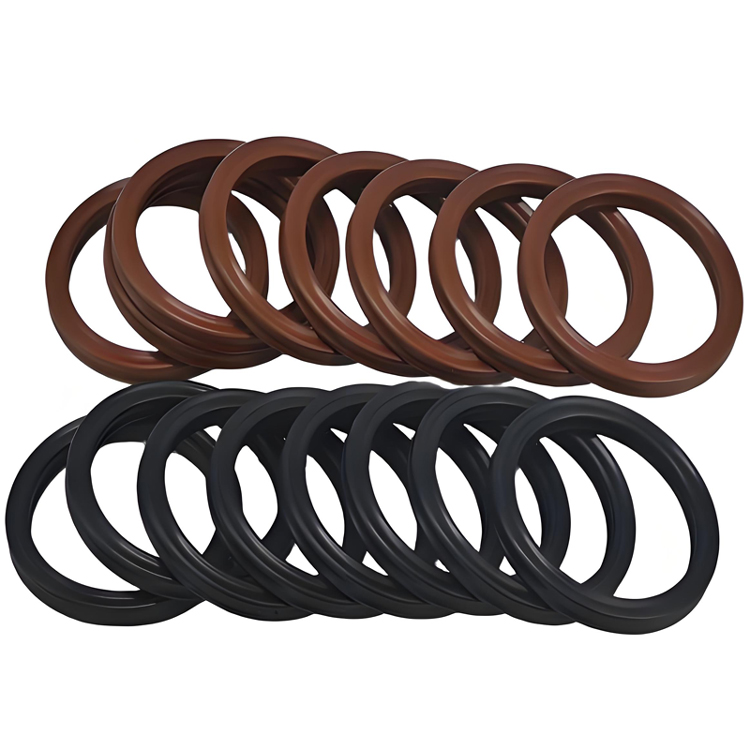
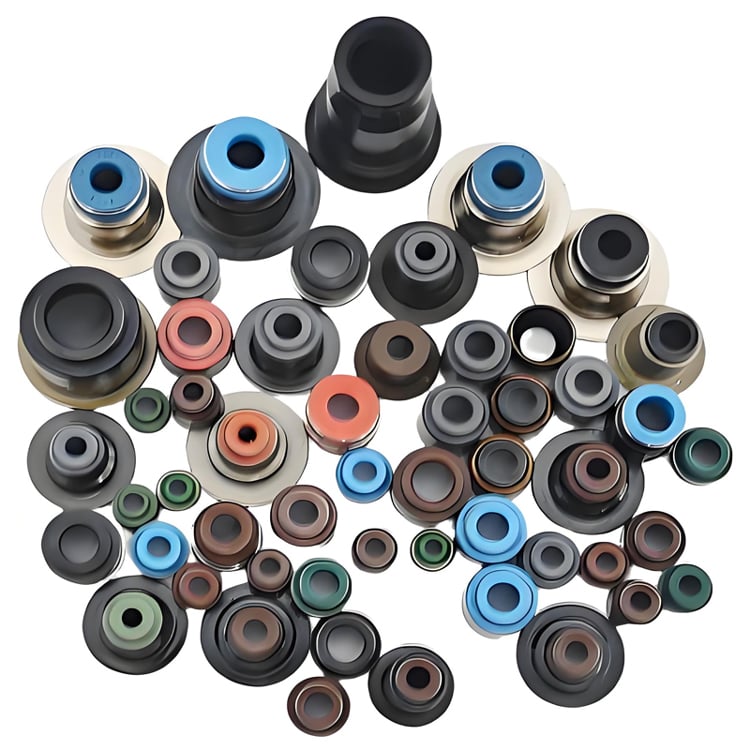
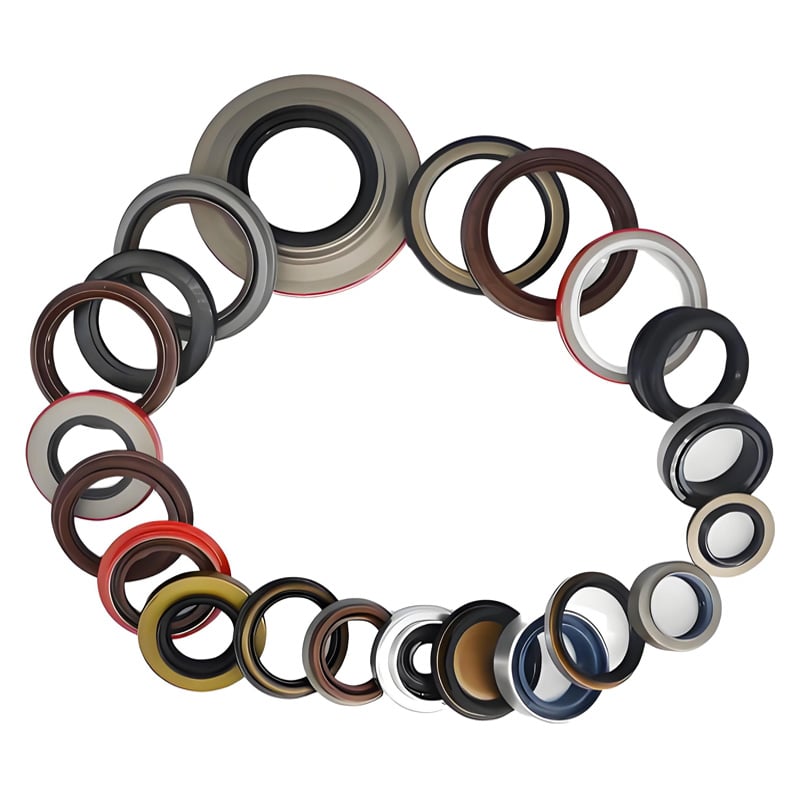
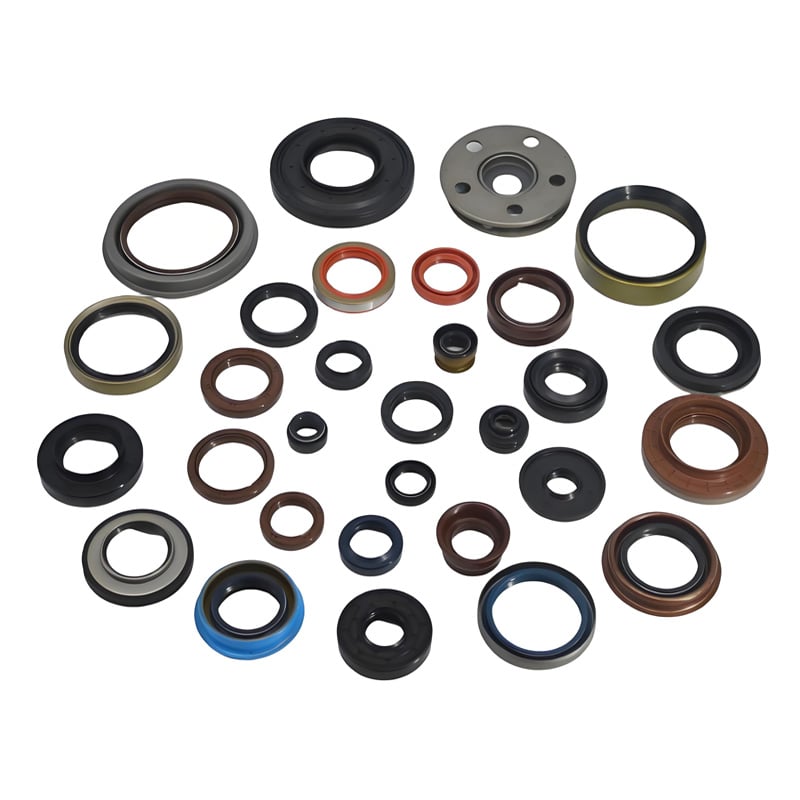
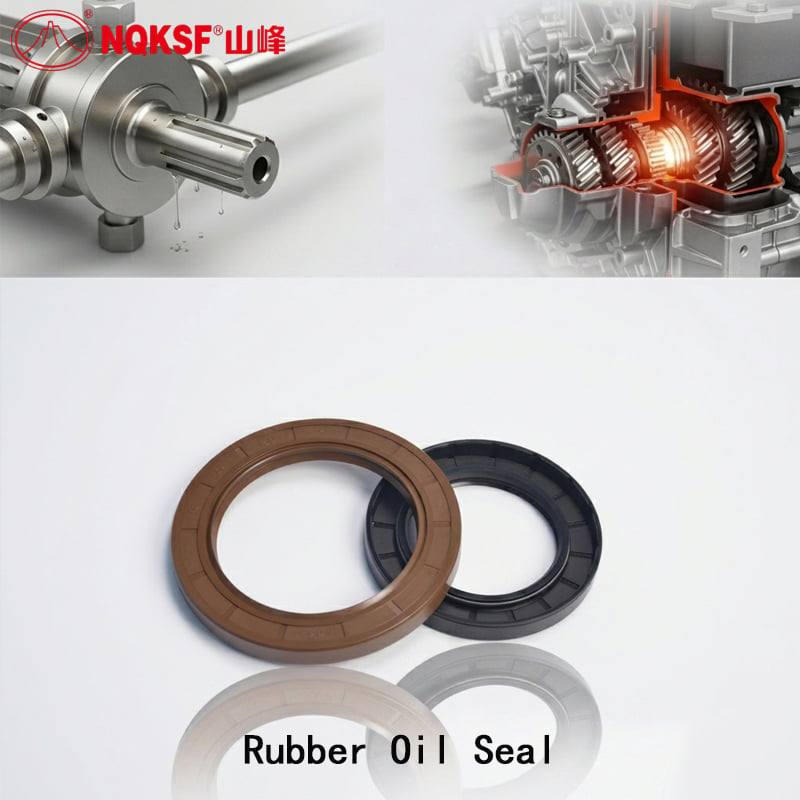
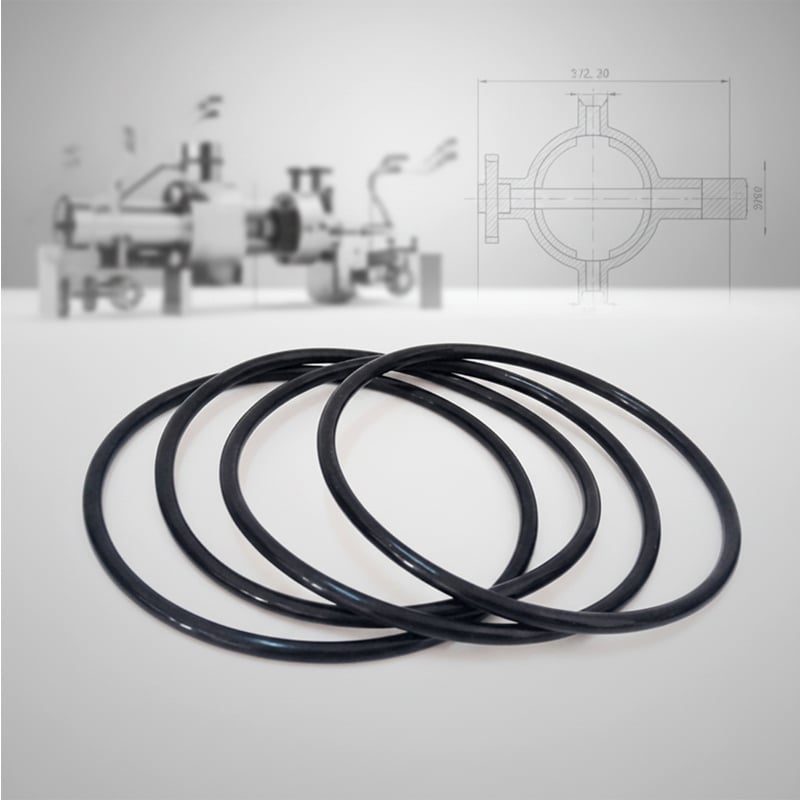
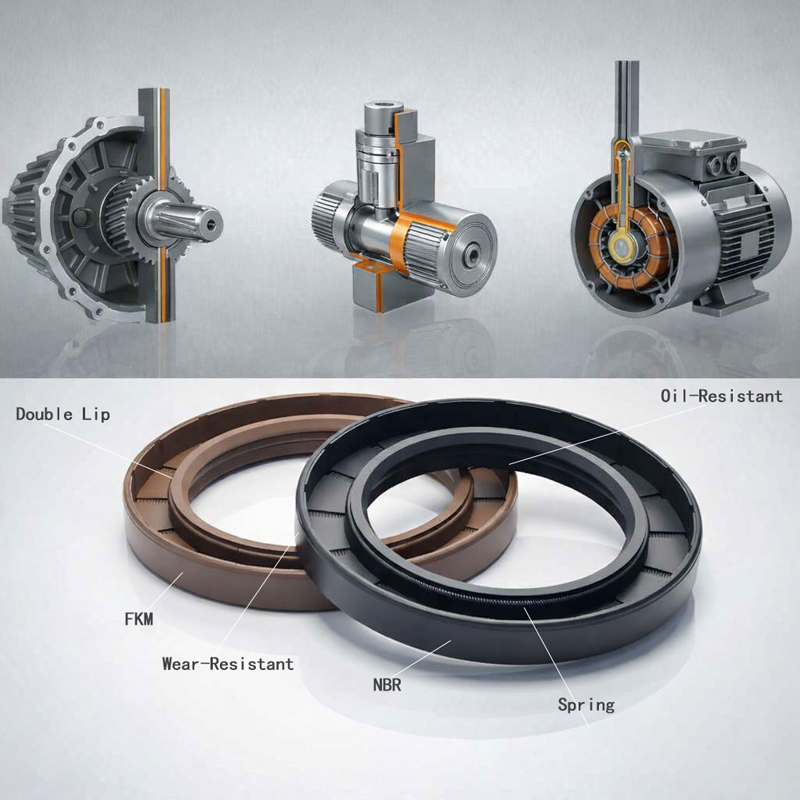
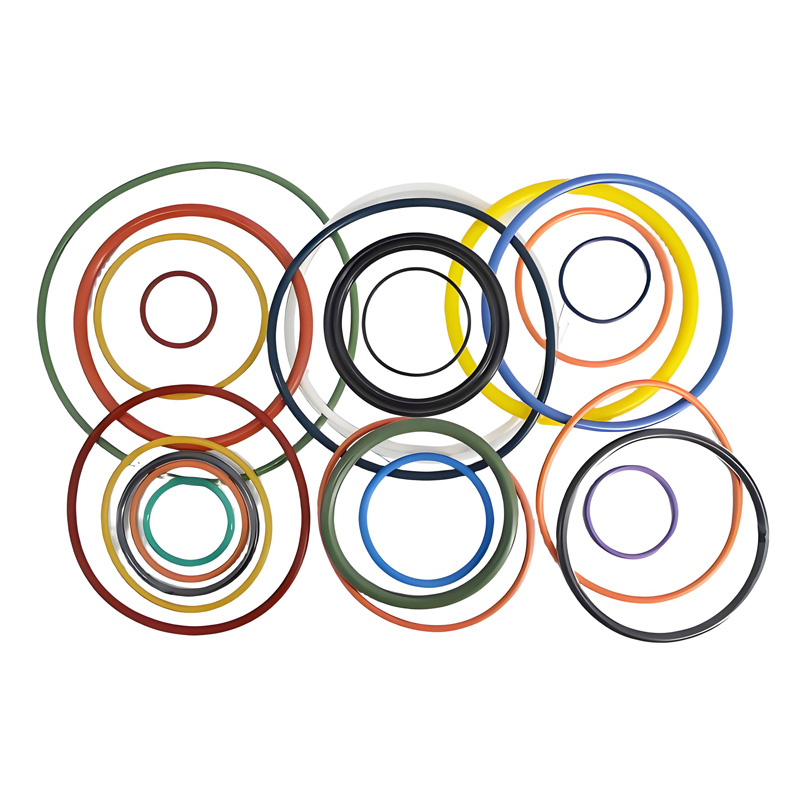
A sealing rubber ring is an essential component designed to create a tight, dependable barrier between two surfaces, preventing liquid or gas leakage in various applications. This sealing rubber ring functions as a critical protective element in mechanical systems, industrial equipment, and domestic appliances. The primary purpose of a sealing rubber ring is to maintain system integrity by blocking unwanted fluid escape or external contamination entry. Modern sealing rubber ring technology incorporates advanced elastomer materials that withstand extreme temperatures, pressure variations, and aggressive chemical environments. The technological features of a quality sealing rubber ring include superior elasticity, exceptional durability, and resistance to degradation. Manufacturers engineer each sealing rubber ring with precision dimensions to ensure perfect fit and maximum sealing efficiency across diverse operating conditions. Applications for a sealing rubber ring span numerous industries. Automotive manufacturers rely on sealing rubber rings in engines, transmissions, and hydraulic systems. Medical device producers use specialized sealing rubber rings to maintain sterility and functionality. Water treatment facilities depend on sealing rubber rings to prevent contamination. Refrigeration units, pumps, compressors, and industrial machinery all require sealing rubber rings for optimal performance. The versatility of sealing rubber rings makes them indispensable in plumbing, HVAC systems, and food processing equipment, where maintaining sealed environments is critical for safety and operational success.
Popular Products

Choosing a high-quality sealing rubber ring delivers substantial practical benefits that directly improve your equipment performance and reduce maintenance costs. These components work quietly and reliably, requiring minimal oversight once installed, allowing your systems to operate smoothly without constant attention or adjustment. Operational benefits of a reliable sealing rubber ring are immediately apparent. Your equipment maintains consistent pressure levels, preventing gradual fluid loss that compromises performance efficiency. This containment capability extends equipment lifespan significantly, protecting internal components from corrosion and damage caused by leakage or contamination. A properly functioning sealing rubber ring eliminates emergency breakdowns, reducing expensive downtime and emergency repair expenses. The practical value extends beyond just leak prevention. Installing a quality sealing rubber ring simplifies maintenance routines, as fewer service interventions become necessary when systems remain properly sealed. This translates to lower labor costs and reduced operational disruptions. Your facility experiences improved safety conditions because contained systems prevent hazardous spills and environmental contamination that could harm workers or damage surroundings. For application suitability, the sealing rubber ring adapts seamlessly across diverse industries and equipment types. Whether you operate automotive facilities, pharmaceutical production lines, or water treatment plants, an appropriately selected sealing rubber ring provides dependable performance. Decision-useful context emerges when comparing total cost of ownership: investing in quality sealing rubber rings upfront prevents expensive damage claims, warranty issues, and production delays. Smart buyers recognize that premium sealing rubber rings deliver superior return on investment through reliability, longevity, and consistent performance across demanding operational environments.

Practical Tips

How to maintain a shaft oil seal in dusty industrial environments?

29

May

How to maintain a shaft oil seal in dusty industrial environments?

Maintaining a shaft oil seal in dusty industrial environments requires specialized attention to contamination prevention and proactive maintenance protocols. Dust infiltration represents one of the most common causes of premature shaft oil seal failu...
View More
Which auto oil seal materials are best for modern transmission fluids?

03

Jun

Which auto oil seal materials are best for modern transmission fluids?

Modern automotive transmissions demand exceptional sealing performance to maintain fluid integrity and prevent costly leakage failures. The selection of appropriate auto oil seal materials has become increasingly critical as transmission fluids evolv...
View More
What are the advantages of using an NBR rubber oil seal in oily media?

03

Jun

What are the advantages of using an NBR rubber oil seal in oily media?

NBR rubber oil seals offer exceptional performance characteristics that make them particularly well-suited for applications involving oily media environments. When industrial equipment operates in conditions where petroleum-based lubricants, hydrauli...
View More
How Do O Ring Seal Differ from Other Sealing Solutions?

22

Jul

How Do O Ring Seal Differ from Other Sealing Solutions?

Understanding the fundamental differences between various sealing solutions is crucial for engineers and procurement professionals making critical design decisions. While multiple sealing technologies exist in the industrial marketplace, the unique c...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Telephone
Name
Company Name
Message
0/1000

sealing rubber ring

Superior Leak Prevention and System Integrity

Superior Leak Prevention and System Integrity

A high-performance sealing rubber ring creates an impenetrable barrier that prevents fluid loss and maintains system pressure consistently. This fundamental capability distinguishes quality sealing rubber rings from inferior alternatives. When your equipment relies on a robust sealing rubber ring, you eliminate the gradual pressure drops that compromise efficiency and reduce operational lifespan. The sealing rubber ring accomplishes this through precise geometry and advanced elastomer composition that conforms perfectly to mating surfaces. This conformability ensures that your sealing rubber ring maintains its seal across temperature fluctuations and pressure variations that would deteriorate ordinary gaskets. By investing in premium sealing rubber rings, you protect valuable equipment from internal damage caused by fluid contamination or external element intrusion. Industrial managers recognize that a dependable sealing rubber ring represents excellent insurance against costly equipment failures and production delays.
Extreme Durability and Extended Component Lifespan

Extreme Durability and Extended Component Lifespan

Professional-grade sealing rubber rings demonstrate exceptional resistance to environmental stressors that typically degrade standard gaskets. The advanced materials used in quality sealing rubber rings withstand extreme temperature ranges, aggressive chemical exposures, and intense pressure conditions without losing effectiveness. Your sealing rubber ring maintains elasticity and flexibility throughout its operational life, preventing the brittleness that causes premature failure in competing products. This durability advantage means your sealing rubber ring continues performing reliably for years longer than conventional alternatives, dramatically improving your equipment's total cost of ownership. The superior engineering in each sealing rubber ring ensures consistent performance across thousands of operational cycles without degradation. Whether your sealing rubber ring operates in freezing industrial environments or extreme heat applications, premium elastomer formulations preserve functionality and leak-prevention capability. Equipment managers consistently report that upgrading to high-quality sealing rubber rings significantly reduces replacement frequency and associated maintenance expenses.
Versatile Compatibility Across Multiple Applications

Versatile Compatibility Across Multiple Applications

Quality sealing rubber rings adapt seamlessly to diverse equipment types, industries, and operational environments, offering exceptional versatility. Your sealing rubber ring performs reliably in automotive engines, refrigeration systems, medical devices, water treatment facilities, and industrial machinery. This broad compatibility means a single sealing rubber ring specification can serve multiple applications, simplifying inventory management for multi-operation facilities. The universal design principles underlying premium sealing rubber rings ensure perfect integration with existing equipment without modification or adaptation. Technical specifications for each sealing rubber ring are carefully engineered to accommodate standard international dimensions, promoting interchangeability and reducing procurement complexity. Whether you require a sealing rubber ring for agricultural equipment, pharmaceutical production, or aerospace applications, appropriate options exist within quality product lines. This versatility provides procurement flexibility and operational continuity, allowing your organization to standardize on reliable sealing rubber ring products across diverse equipment portfolios.

Get a Free Quote

Our representative will contact you soon.
Email
Telephone
Name
Company Name
Message
0/1000