Oil Ring Seals: Premium Fluid Containment

All Categories

oil ring seals

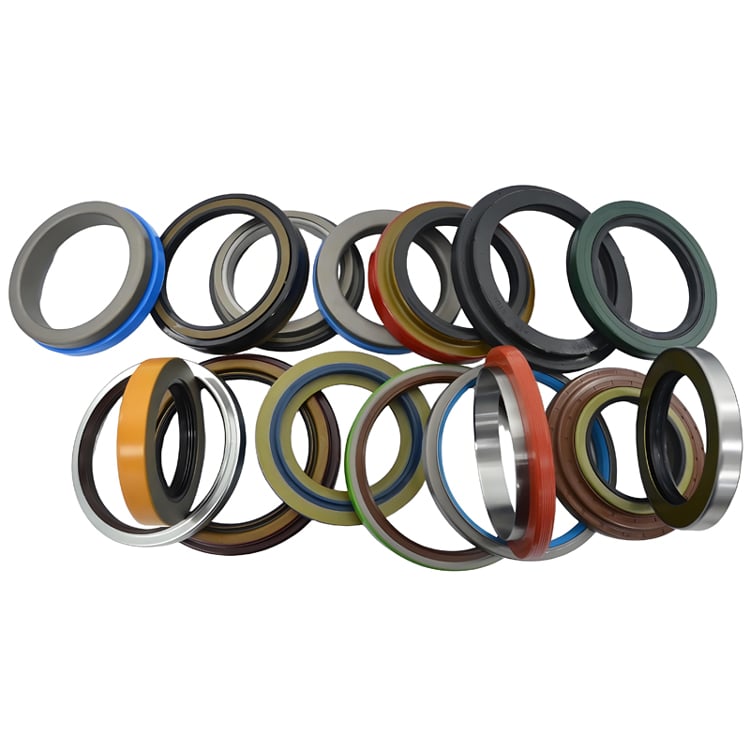
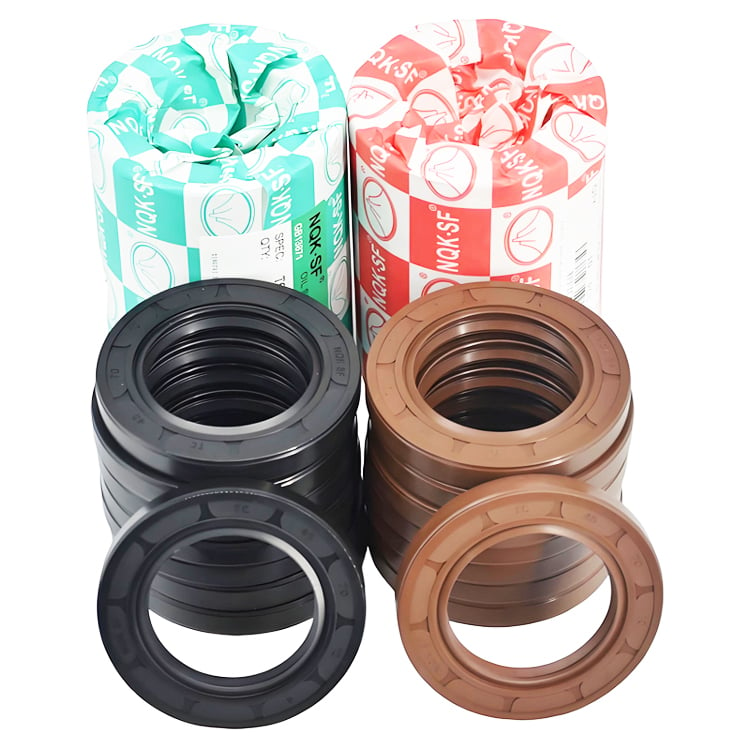
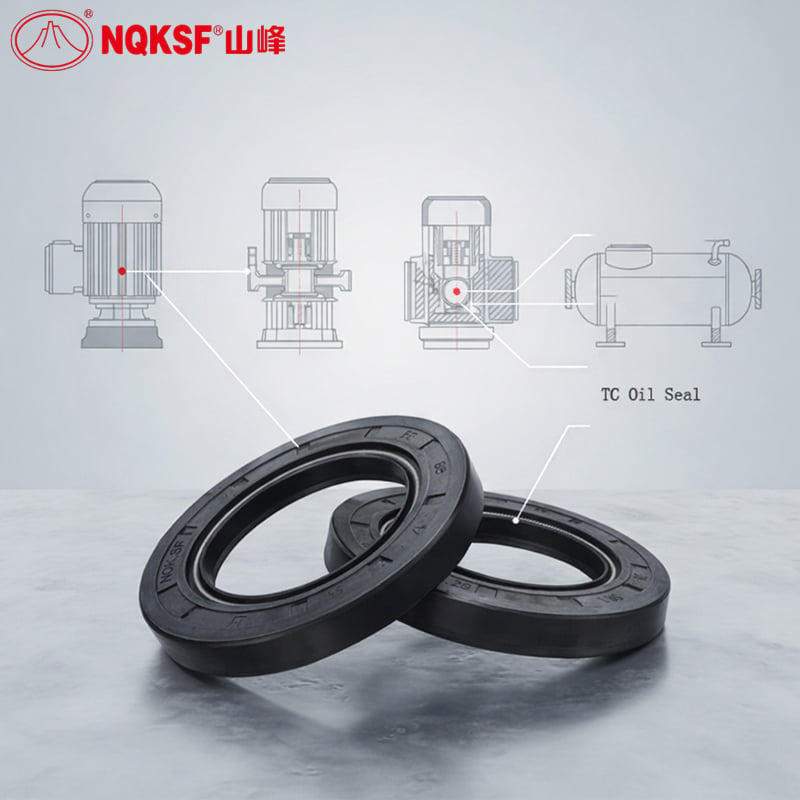
Oil ring seals are essential mechanical components designed to prevent fluid leakage while maintaining optimal pressure within rotating equipment systems. These specialized seals function as a critical barrier between moving and stationary parts, ensuring the integrity of hydraulic systems, pumps, and industrial machinery. Oil ring seals work by creating a dynamic seal that adapts to micro-movements and surface irregularities, providing superior protection against oil escape and contamination ingress. The primary function of oil ring seals involves maintaining consistent lubrication flow while preventing unwanted fluid escape. Oil ring seals accomplish this through their engineered elastomer materials and precision-designed geometries that conform to equipment specifications. These seals feature advanced technological innovations including reinforced core structures and specialized surface treatments that enhance durability and performance under demanding conditions. Oil ring seals find extensive applications across diverse industries including automotive manufacturing, hydraulic equipment production, compressor systems, and heavy machinery operations. The versatility of oil ring seals makes them indispensable in environments where fluid containment and operational reliability are paramount. Modern oil ring seals incorporate cutting-edge materials science, enabling them to withstand extreme temperatures, high-pressure scenarios, and aggressive chemical exposures. Technological features of oil ring seals include precision tolerance manufacturing, multi-directional sealing capabilities, and enhanced friction resistance. These characteristics ensure that oil ring seals maintain consistent performance throughout their operational lifespan, reducing maintenance interruptions and extending equipment service intervals significantly.
New Product Recommendations

Oil ring seals deliver substantial practical benefits that enhance equipment reliability and operational efficiency across multiple industrial applications. The primary advantage lies in their proven ability to eliminate costly fluid leaks that compromise system performance and create environmental hazards. Organizations implementing quality oil ring seals experience dramatically reduced maintenance downtime and extended equipment lifecycle duration. From an operational perspective, oil ring seals provide consistent pressure retention, enabling machinery to function at peak efficiency without energy losses attributable to fluid escape. This performance characteristic directly translates into measurable cost savings through reduced fluid replacement cycles and minimized contamination-related breakdowns. Equipment operators appreciate how oil ring seals maintain stable operating conditions, preventing temperature fluctuations and pressure inconsistencies that damage sensitive machinery components. The application suitability of oil ring seals spans virtually every industrial sector requiring fluid containment solutions. Whether protecting hydraulic systems in construction equipment, sealing automotive engine components, or maintaining pressure in manufacturing facilities, oil ring seals deliver dependable results. Their compatibility with diverse fluid types and operating temperatures makes oil ring seals the preferred choice for engineers designing reliable systems. Decision-useful product context demonstrates that selecting premium oil ring seals represents intelligent long-term investment strategy. Superior oil ring seals minimize replacement frequency, reduce warranty claims, and enhance overall system reliability metrics. Customers purchasing authentic oil ring seals from reputable manufacturers gain confidence in equipment dependability, knowing that fluid containment challenges have been professionally addressed through engineered excellence.

Tips And Tricks

Why is material hardness vital for a hydraulic oil seal under pressure?

11

Aug

Why is material hardness vital for a hydraulic oil seal under pressure?

Material hardness stands as one of the most critical factors determining whether a hydraulic oil seal can withstand extreme pressures and maintain system integrity over time. When hydraulic systems operate at high pressures, seals face tremendous mec...
View More
What Are the Key Applications of Shaft TC Oil Seals?

29

May

What Are the Key Applications of Shaft TC Oil Seals?

Shaft TC oil seals serve as critical sealing components in rotating machinery applications across countless industries, where their primary function involves preventing lubricant leakage while blocking external contaminant ingress. These precision-en...
View More
How Do TC Oil Seals Compare to Other Seal Types?

03

Jun

How Do TC Oil Seals Compare to Other Seal Types?

Understanding the differences between TC oil seals and other seal types is crucial for engineers and maintenance professionals selecting the right sealing solution for their applications. TC oil seals, also known as rotary shaft seals or lip seals, r...
View More
How Do O Ring Seal Differ from Other Sealing Solutions?

22

Jul

How Do O Ring Seal Differ from Other Sealing Solutions?

Understanding the fundamental differences between various sealing solutions is crucial for engineers and procurement professionals making critical design decisions. While multiple sealing technologies exist in the industrial marketplace, the unique c...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Telephone
Name
Company Name
Message
0/1000

oil ring seals

Superior Leak Prevention Technology

Superior Leak Prevention Technology

Oil ring seals incorporate advanced elastomer compounds and precision engineering that creates an impenetrable barrier against fluid escape. This leak prevention capability directly protects equipment investments by preventing costly fluid loss and system contamination. The sophisticated design of oil ring seals ensures contact surfaces remain sealed even during micro-movements and thermal fluctuations inherent in industrial operations. Organizations implementing high-quality oil ring seals experience elimination of oil seepage problems that plague inferior alternatives. The technological superiority embedded within oil ring seals reflects decades of mechanical engineering innovation focused on maximum reliability. This advantage becomes particularly evident in demanding applications where equipment operates continuously under elevated pressure conditions, making oil ring seals the engineered solution for uncompromising performance standards.
Extended Equipment Service Life

Extended Equipment Service Life

Premium oil ring seals significantly extend machinery operational lifespan by protecting internal components from contamination and maintaining optimal lubrication conditions. The durability characteristics of quality oil ring seals reduce replacement frequency and associated operational disruptions. By preventing premature wear caused by fluid escape and contamination ingress, oil ring seals protect expensive machinery components from degradation. Organizations benefit from maximized equipment investment value when implementing superior oil ring seals within their operational infrastructure. The long-term financial implications of choosing robust oil ring seals include reduced capital expenditure on replacement equipment and diminished maintenance labor requirements. Extended service intervals possible with properly functioning oil ring seals translate into substantial operational cost reductions throughout equipment lifespan, making this investment decisively economical.
Reliable Performance Under Demanding Conditions

Reliable Performance Under Demanding Conditions

Oil ring seals maintain consistent sealing integrity across extreme operating environments, including elevated temperatures, high-pressure scenarios, and exposure to aggressive chemical exposures. The advanced material composition of modern oil ring seals enables reliable performance where inferior alternatives fail catastrophically. This dependability characteristic makes oil ring seals indispensable for critical applications where system failure creates safety hazards or production delays. The robust engineering inherent within quality oil ring seals ensures stable operation during thermal cycling and mechanical stress conditions. Industries requiring absolute reliability increasingly specify premium oil ring seals to guarantee uninterrupted equipment functionality. The proven performance history of engineered oil ring seals across diverse challenging applications demonstrates their superiority and justifies specification choices made by discerning equipment manufacturers and maintenance professionals worldwide.

Get a Free Quote

Our representative will contact you soon.
Email
Telephone
Name
Company Name
Message
0/1000