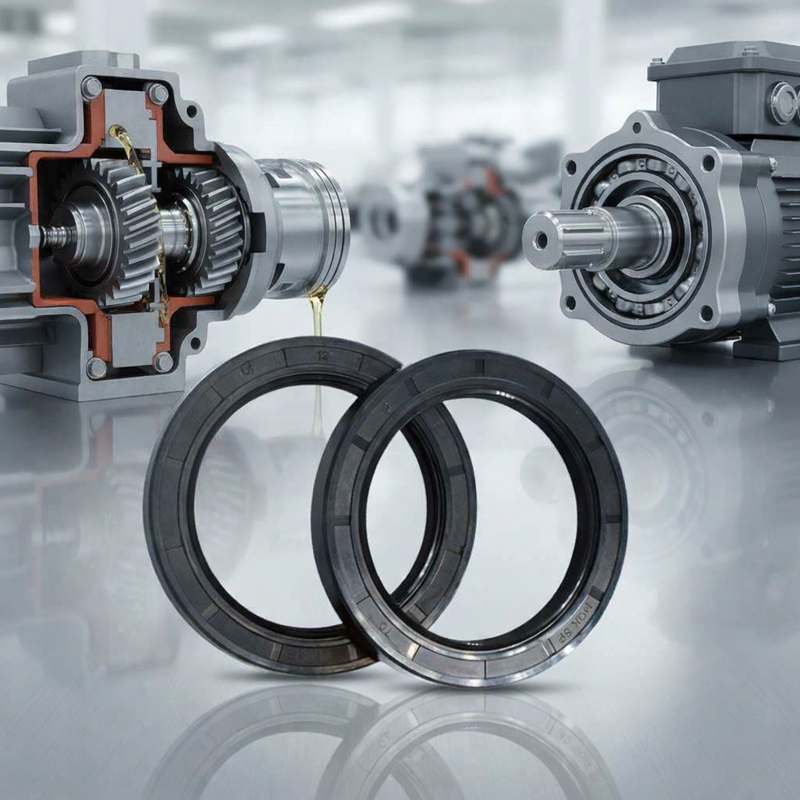
quality oil seal
A quality oil seal represents a critical component in machinery and equipment systems, designed to prevent fluid leakage while maintaining operational integrity. This precision-engineered device functions as a barrier between moving and stationary parts, effectively containing lubricating oils, hydraulic fluids, and other essential liquids within their designated chambers. The quality oil seal serves multiple vital functions in industrial and automotive applications, ensuring that machinery operates smoothly without costly fluid loss or contamination.
The primary function of a quality oil seal is to create an impermeable barrier that stops oil from escaping past rotating shafts or moving components. By maintaining proper fluid retention, a quality oil seal prevents environmental contamination and protects surrounding machinery from damage caused by leaked fluids. This component utilizes advanced elastomeric materials and precision manufacturing techniques to deliver exceptional performance under extreme temperatures, pressures, and rotational speeds.
Technologically, modern quality oil seal designs incorporate sophisticated features including dual-lip configurations, reinforced spring mechanisms, and specialized coating treatments. These innovations enable the quality oil seal to withstand harsh operating conditions while maintaining a consistent seal over extended periods. The engineering behind a quality oil seal ensures minimal friction, reduced energy consumption, and extended equipment lifespan.
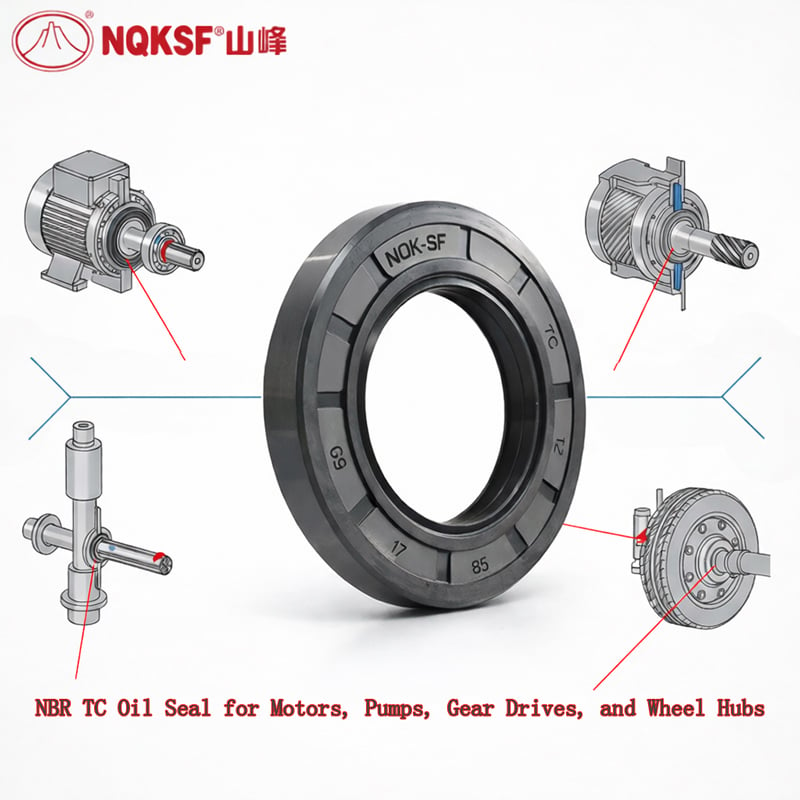
Applications for quality oil seal technology span numerous industries including automotive engines, industrial pumps, hydraulic systems, compressors, and transmission systems. Whether in heavy machinery, agricultural equipment, or precision manufacturing facilities, the quality oil seal remains indispensable. Its reliability directly impacts equipment performance, maintenance costs, and overall operational efficiency across diverse sectors.
 EN